
An industrial nameplate order involves more than printing machine details on a metal sheet. The alloy, marking method, surface treatment, mounting design and inspection plan must match the machine’s environment and the information it must retain. By the end, you will know how to prepare a production-ready order and compare the main manufacturing routes.
Key takeaways
- Approve artwork, machine data and variable numbers before cutting aluminium.
- Choose printing, etching or anodised marking based on wear and legibility needs.
- Match alloy, thickness, finish and adhesive to temperature, humidity and installation.
- Verify dimensions, text, serial numbers and packaging before dispatch.
From approved artwork to cut aluminium sheet
The production sequence begins only after the artwork, machine data and variable-number list are approved. For anyone comparing how aluminium nameplates are made for industrial machinery in Mumbai, the material route must also reflect humidity, monsoon wetting, coastal salt and the machine’s operating temperature.
1. Confirm the approved proof, revision number, reading direction, colours, minimum character height, barcode format, holes, corners and bend lines. Freeze the buyer’s master list of model numbers, ratings and serial numbers.
2. Specify the aluminium alloy, temper, surface condition and thickness, using ASTM B209/B209M as a material reference rather than ordering “aluminium” without detail.
3. Cut sheet or coil to blank size by guillotine, CNC routing, laser cutting or another approved method. Record grain direction when forming or appearance matters.
4. Deburr every edge, remove chips and degrease the surface. Oil left behind can cause ink, paint or adhesive failure.
5. Apply the selected marking process: screen or digital/UV printing, chemical etching with paint fill, engraving, or anodised photo imaging.
6. Cure ink or paint, seal anodised graphics, and add the specified protective overcoat. The process may reverse for certain parts; marking before punching prevents tooling from damaging the finished face.
7. Drill, punch or countersink holes, form bends, and remove new burrs. Check that forming has not cracked the finish.
8. Inspect dimensions, artwork, readability, scratches and coverage; reconcile every serial number against the master list. Pack finished plates with the specified adhesive, liners or fasteners.
Choosing between printing, etching and anodised marking
Abrasion and cleaning solvents rule out unprotected ink. Select the marking system against the actual exposure, not only the artwork or order quantity.
| Method | Abrasion and solvents | Sunlight and heat | Variable data |
|---|---|---|---|
| Anodised or photo-anodised aluminium | Excellent durability because the image is sealed into the anodic layer; strong choice for wiping and solvents | Strong outdoor stability and heat resistance within the alloy and process limits | Suitable for serial numbers, QR codes and barcodes, but allow for setup and verify code contrast |
| Chemical etching with paint fill | Recessed characters resist wiping better than surface-only printing; qualify paint-fill adhesion against the cleaning solvent | Good durability after protective finishing; fine lines can vary through undercutting | Possible for changing data, but slower and less economical for many unique plates |
| Screen printing | Economical for volume orders; abrasion or solvent exposure can remove ink unless the ink and clear coat pass testing | Depends on the ink and overcoat; do not assume outdoor or heat resistance | Works for bold colours and simple variable fields |
| Digital or UV printing | Fast for short runs and changing artwork; needs a qualified protective clear coat | UV resistance and heat performance depend on ink and coating | Best for frequent serial, QR-code or barcode changes |
The aluminium nameplates production process in Mumbai should include a solvent-rub and abrasion test using the buyer’s actual cleaner. For variable codes, specify the minimum X-dimension, quiet zone, contrast and verification grade; a code that looks sharp can still fail on reflective aluminium or beneath a glossy clear coat.
Turning a machine data sheet into a production drawing
A data sheet is not a production drawing: it names the machine, but does not tell a fabricator where holes go or how small lettering may be. Approve a dimensioned drawing and artwork proof before material is cut for custom aluminium nameplates for machinery.
1. Lock the identification content: model, serial number, rated voltage, current, power, frequency, phase, weight, manufacturer, manufacturing date and required warning symbols.
2. Dimension the plate’s overall length and width, thickness, border, corner radius, hole or slot diameter, centre positions, countersinks, adhesive area and any bend lines. Include bend allowance where the plate will be formed.
3. Set legibility limits: minimum character height, minimum line width, font, logo geometry, barcode symbology, quiet zone and reading direction after installation.
4. Approve colour references, marking method, background and protective finish against a named colour standard or physical proof. A vector file alone does not define manufacturing tolerances.
5. Define variable data rules, including serial-number format, character count, barcode-to-serial match, permitted symbols, starting number and buyer’s master list. Add the drawing number, revision, date and approval signature.
The drawing must also identify alloy, temper, thickness and surface condition; “aluminium” is insufficient. If applicable, cite ASTM B209/B209M and state thickness tolerance. Approve the first-article layout before the full run, because an attractive plate with misplaced holes, unreadable text or a reversed barcode becomes scrap after marking and forming.
Matching alloy, thickness, finish and adhesive to the installation
A 0.5 mm 5052-H32 plate suits a flat indoor panel; a thicker plate resists bending on a machine frame, while a thin plate follows a slight curve. Specify alloy, temper, thickness tolerance and surface condition under ASTM B209/B209M, not merely “aluminium.”
| Choice | Effect on performance | Specify it when |
|---|---|---|
| 5052-H32 | Good corrosion resistance, stiffness and formability | The plate faces humidity, monsoon wetting, salt air or light forming |
| 0.5–1.0 mm thickness | Thinner stock lowers weight; thicker stock stays flatter and handles better | Match thickness to plate size, unsupported span and mounting holes |
| Anodised finish | Harder, more abrasion-resistant surface with durable contrast; scratches can still expose the substrate | Sunlight, handling or cleaning threatens legibility; request an agreed test and reference ISO 7599 |
| Screen, UV or etched marking | Printing supports colour and variable data; etching with paint fill withstands abrasion after correct sealing | Select against solvent, heat, sunlight and required traceability |
| Acrylic pressure-sensitive adhesive | Bonds quickly to a clean, smooth surface; failure follows oil, dust, condensation or rough texture | Use on flat panels after cleaning and confirm service temperature and humidity |
| Mechanical fixing | Prevents adhesive failure but needs holes, clearance and sealing against water behind the plate | Vibration, heat, curved surfaces or contaminated paint make adhesive unreliable |
The aluminium nameplate manufacturing steps must preserve the chosen face: mark or anodise before punching when tooling could scratch it, then deburr, clean, cure or seal, and inspect. For outdoor or coastal installation, specify edge protection and a layout that prevents water pooling behind the plate.
Inspecting, verifying and packing the finished order
Confirm the finished order against the approved drawing, identification data, marking method, installation details and packing specification before release. A readable plate with the wrong serial number is still a failed order.
Use a numbered inspection record:
1. Match the revision number, machine model, serial-number sequence, ratings, warning symbols, logo and manufacturing details against the approved artwork. Quarantine any plate with a missing character, transposed digit or outdated revision.
2. Measure overall length, width, thickness, corner radius, hole diameter and hole centres. Check bends, countersinks and burrs against the drawing; a misplaced hole can make a correct plate impossible to install.
3. Inspect text, barcodes and symbols under normal viewing distance and expected lighting. Check small characters for filled counters, broken strokes, colour mismatch and poor contrast, then scan variable-data codes if the order requires traceability.
4. Confirm that the specified finish is present and undamaged. For photo-anodised plates, verify that the image is sealed; for printed plates, check curing and resistance to the agreed rub, solvent or abrasion test.
5. For industrial aluminium labels in Mumbai, record the agreed corrosion and legibility test for humidity, monsoon wetting, salt exposure or condensation. “Outdoor grade” alone is not a test specification.
6. Check adhesive type, liner condition and fastener pack against the substrate, temperature, oil exposure and plate size. Protect the face, prevent water collection behind the plate, separate stacked parts and mark cartons with quantity, part number and revision.
Shreeniwas Signs Pvt Ltd can use this record to prevent packing a visually acceptable plate whose adhesive, holes or identification data fail at installation.
Related products
 | Metal Labels Aluminum Nameplates are popularly known for their light weight and capacity to oppose corrosion.Its recognizable gleaming white shine offers... View product → |
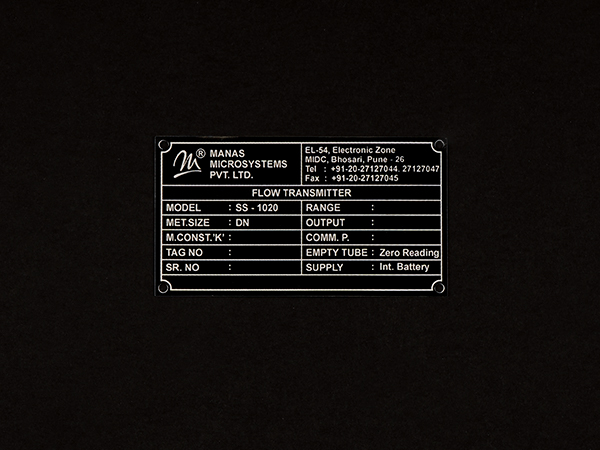 | Metal Labels Machine Specification Nameplate A Machine Specification Nameplate distinguishes and shows an item's name on gadget. View product → |
Frequently asked questions
What happens before aluminium nameplate production begins?
The manufacturer confirms approved artwork, machine data and the variable-number list before preparing the production drawing and cutting aluminium sheet.
How do you choose between printed, etched and anodised aluminium marking?
Compare the marking method with the required wear resistance, contrast, environmental exposure and level of variable information.
What details belong in a machinery nameplate production drawing?
Include the nameplate dimensions, hole positions, corner treatment, text and symbols, serial or rating data, material, finish, adhesive and artwork revision.
How should aluminium nameplates be matched to their installation?
Select the alloy, thickness, surface finish and adhesive for the machine surface, operating temperature, humidity, monsoon wetting and coastal salt exposure.
What should you inspect before packing finished nameplates?
Check dimensions, holes, edges, finish, legibility, artwork revision, serial numbers and quantity, then protect the plates from scratching during packing.